Explore our precision-engineered display systems and heavy-duty shelving solutions built to international quality standards.
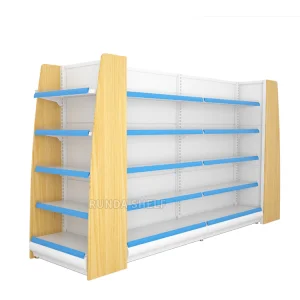
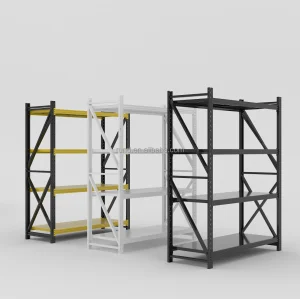
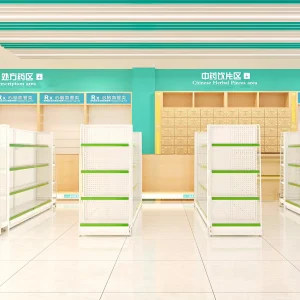
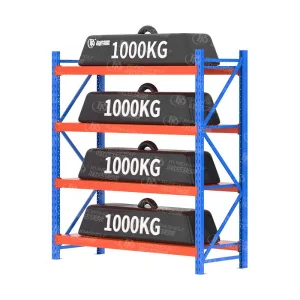
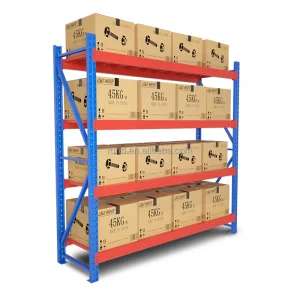
Founded in 2016, Suzhou Expandrack Logistics Equipment Co., Ltd. is a technologically advanced manufacturer specializing in heavy-duty selective pallet racking, drive-in systems, and automated rack-supported warehouse structures.
Backed by 10 years of deep industry expertise and 7 years of seamless international trade background, Suzhou Expandrack operates out of a state-of-the-art facility in Suzhou, China. Driven by rigorous international standards, our company consistently delivers excellence across global supply chain networks.
Our engineering prowess bridges the gap between raw metal fabrication and intelligent commercial merchandising infrastructure, providing global distributors with unmatched structural integrity and thermal optimization solutions.
Delivering robust, certified display and storage solutions worldwide to support critical commercial ecosystems.
Our global market presence strategically spans Southeast Asia, the Middle East, South America, and Eastern Europe, meeting localized regulatory and climatic demands.
Leveraging a resilient supply chain of over 850 strategic material and hardware partners, Expandrack delivers end-to-end storage and display solutions tailored for diverse commercial sectors.
Our main customer types include industrial material handling distributors, retail logistics hubs, pharmaceutical storage managers, and automotive assembly lines requiring precision equipment.
Analyzing the macroeconomic shifts in global retail, cold chain technology, and why Chinese industrial clusters lead the export market.
Modern supermarkets and convenience stores are shifting toward IoT-enabled, energy-efficient refrigerated display cases. Integration of variable-speed compressors and eco-friendly refrigerants (R290/CO2) defines the future of sustainable retail.
Suzhou stands as a global hub for advanced metal manufacturing and precision engineering. Proximity to advanced port facilities and an integrated supply chain allows us to deliver high cost-performance ratios without compromising quality.
International buyers demand CE certification, strict thermal performance validation, robust structural corrosion resistance, and customized dimensions to fit varied floor plans across hypermarkets and specialty pharmacies.
Our manufacturing plant operates under stringent ISO 9001:2015 and RMI protocols, backed by a specialized internal laboratory managed by 32 senior QC inspectors.
Strict testing of structural steel raw material grade compliance to ensure maximum load-bearing and thermal endurance.
Continuous online visual laser scanning for upright roll-forming and chassis precision.
Destructive load-to-failure testing on structural beams, shelves, and connector hooks to guarantee absolute safety margins.
Impact and scratch-resistance testing for powder-coated and anti-corrosive stainless steel surfaces.
Our technical center is staffed by 42 specialized structural engineers who design space-optimizing layouts and high-performance commercial refrigerated display systems.
Adjustable pitch spacing, custom column guard designs, and dedicated racking row spacers engineered for optimal airflow and product visibility.
Special frame height configurations up to 15 meters for narrow-aisle (VNA) operations and high-density distribution centers.
Multi-tier mezzanine floor integration and integrated wire mesh decking options to maximize vertical retail and warehouse space.
State-of-the-art production lines equipped with automated shearing, bending, punching, welding, and electrostatic powder-coating technologies.
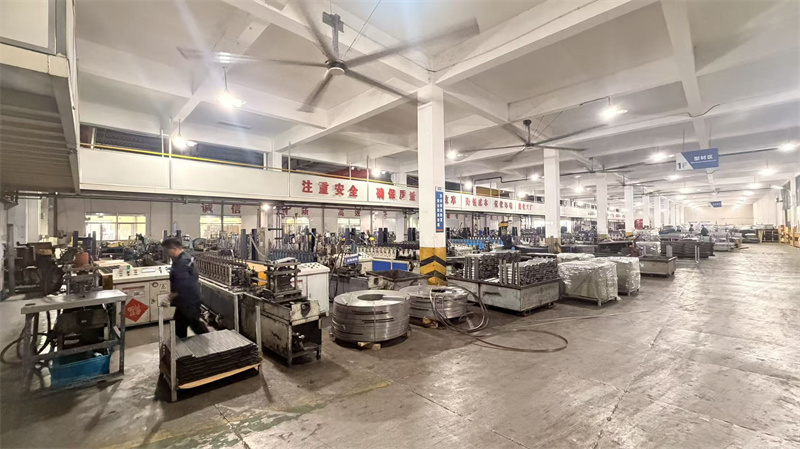
High-precision raw material blanking for structural perfection.
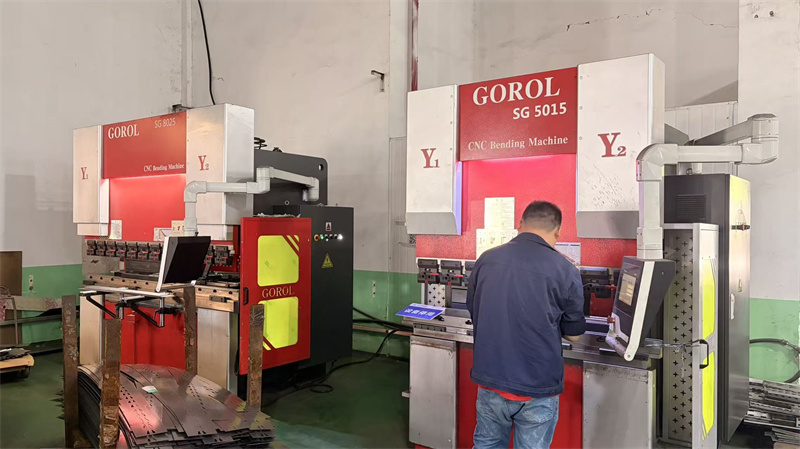
Advanced CNC bending machines ensuring uniform component angles.
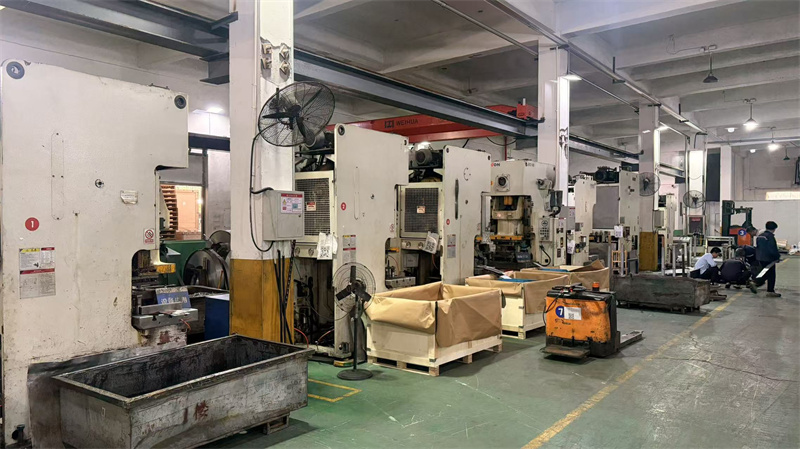
Accurate hole-punching for seamless assembly and adjustability.
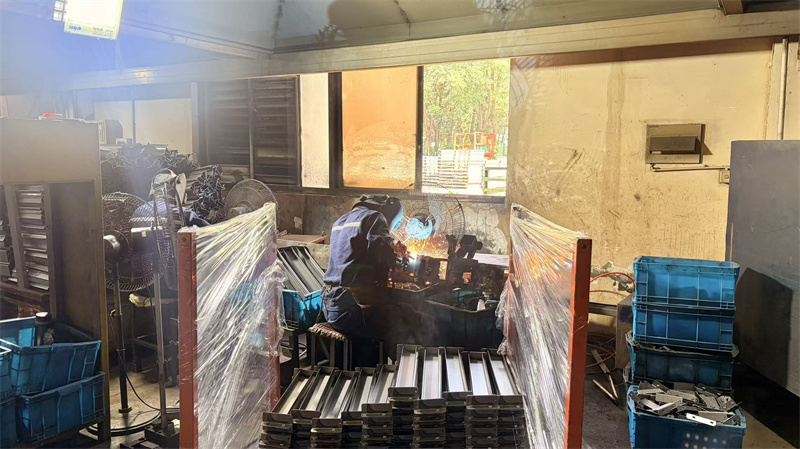
Robotic and certified manual welding for ultimate structural strength.
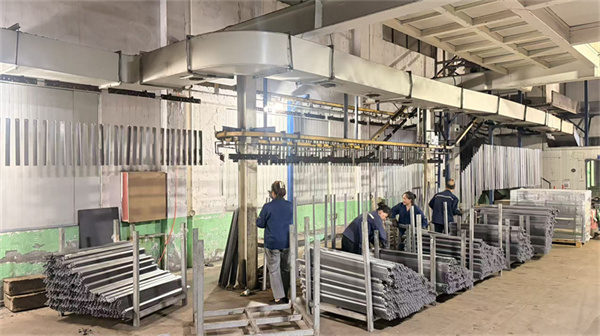
Eco-friendly electrostatic powder coating line for lasting finish.
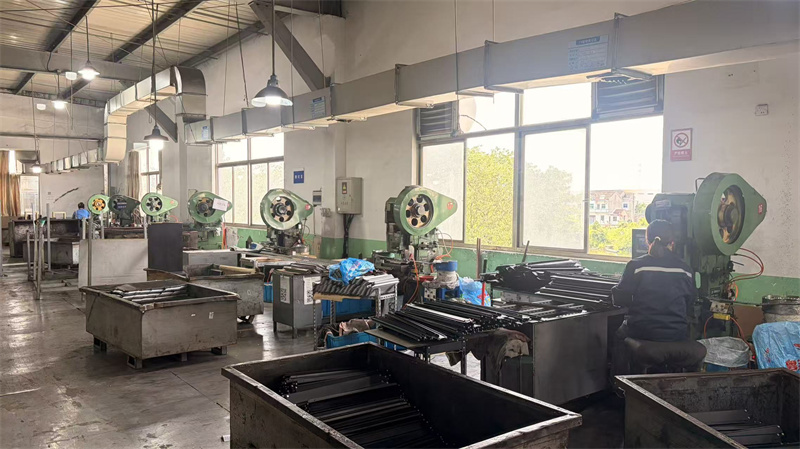
Secure fastening systems for modular stability.
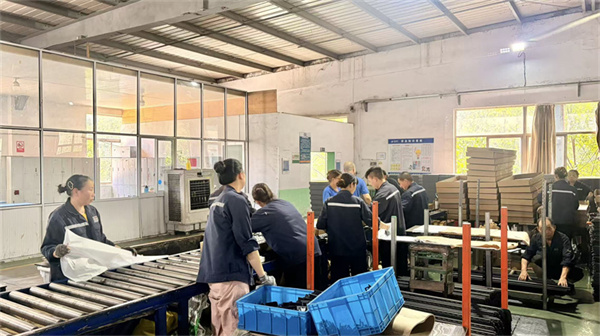
Rigorous final quality checks and export-grade protective packaging.
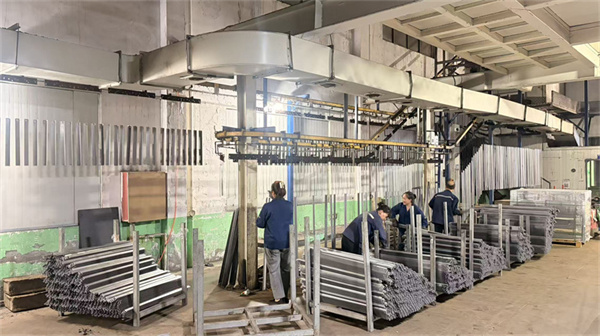
Automated coating tunnels for uniform anticorrosive protection.
Expert answers regarding international procurement, certifications, customization, and logistical support for refrigerated display cases and storage solutions.
All our products are manufactured under strict ISO 9001:2015 quality management systems and comply with international CE safety and performance standards, ensuring smooth customs clearance and regulatory compliance worldwide.
Yes. With an in-house R&D team of 42 engineers, we specialize in OEM/ODM solutions, offering customized pitch spacings, color finishes, frame heights up to 15 meters, and specialized layout configurations.
Standard production cycles range between 20 to 35 days depending on the order volume and customization complexity. Our 42,000-square-meter facility in Suzhou ensures high output capacity and timely delivery.
Our quality control protocol is managed by 32 senior QC inspectors utilizing spectro-analysis, online laser scanning, destructive load testing, and rigorous surface scratch-resistance assessments.
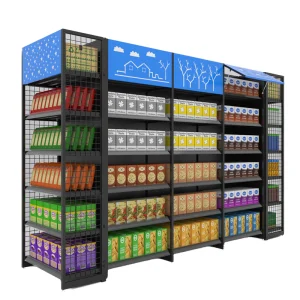
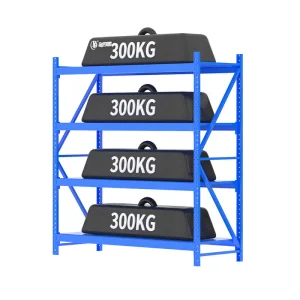
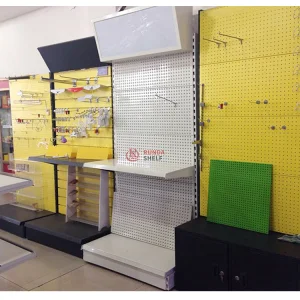
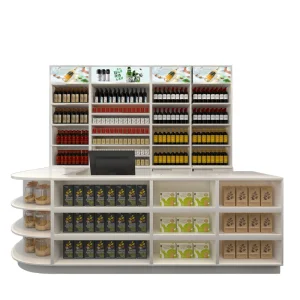
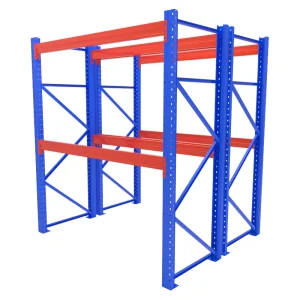
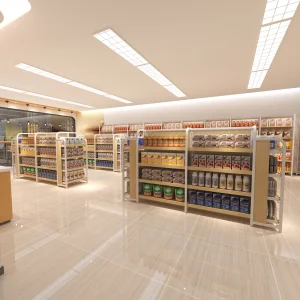
Discover additional industrial storage racks, cash counters, and specialized retail display units designed for global wholesalers.
 Expandrack